Kuehne+Nagel: Building a High-Efficiency Supply Network Across 300+ Suppliers to Support Automotive 4PL Operations
Kuehne+Nagel implemented the HUIPAI SCP solution to unify order, procurement, transportation, and warehouse operations on a single platform. Through Dynamic MRP, inventory verification, and progress tracking, the company optimized end-to-end supply chain operations, improving supply responsiveness and material availability while accelerating the growth of its automotive 4PL business.
45% improvement in supply chain efficiency — Enabled efficient collaboration across 300+ suppliers
28% increase in material availability — Optimized material supply across 6 warehouses and 14 plants
Ningbo Electionics: Accelerating Manufacturing DX Through Legacy Equipment Data Utilization
Ningbo Electionics implemented a Digital Management System and Andon System to collect data from legacy equipment through a proprietary data acquisition method. By enabling one-touch abnormality reporting, the company significantly improved issue reporting efficiency. Enhanced equipment visibility and shop floor improvement initiatives accelerated the digital transformation of manufacturing operations.
60% improvement in abnormality reporting efficiency
Reduced manual reporting through one-touch notifications
20% increase in overall equipment utilization
SANY : Building Smart Factories Through End-to-End Manufacturing Digitalization
SANY implemented the HUIPAI MES solution to accelerate smart factory transformation by integrating digital technologies with manufacturing operations. From workforce management and production planning to execution, logistics distribution, and work instructions, the company achieved end-to-end process visibility, standardization, and digitalization. A data-driven production management framework further improved operational efficiency and decision-making speed.
ALNB: Digitalized Warehousing, Scannable, Traceable, and Precisely Deliverable
ALNB Ningbo Factory has implemented a digital warehouse management system by deeply integrating barcode/RFID technology with automation strategies, enabling rapid identification and dynamic tracking of thousands of materials. The project breaks down information silos and seamlessly integrates with ERP/MES systems, ensuring precise delivery of raw materials to the production line according to the production rhythm. This significantly enhances supply chain responsiveness and warehouse operational efficiency, laying a solid foundation for advancing toward smart warehousing.
Inventory Accuracy Increased to 99.5% 丨 Reduced Inventory Occupancy by 15-20%
 Manufacturing DXBuilt on real manufacturing experience, our smart factory solutions help improve operations and deliver lasting value.

 Products & Services
 HUIPAI APSDriven by on-site needs and business-centric, we precisely address the production-sales coordination and delivery challenges faced by manufacturing enterprises!

 S&OPIntegrate the entire process of demand, supply, production, and delivery to achieve supply-demand balance, capacity optimization, and agile decision-making.
 SCPConnect the demand, inventory, supply, and production collaboration links to achieve complete kit assurance, inventory optimization, and supply resilience.
 DPSDynamically coordinate human, machine, and material resources to quickly respond to order changes, improving capacity utilization and on-time delivery rates.
 Automotive Testing ServicesCovering 4 levels and 8 dimensions, it comprehensively perfects the testing system and process to ensure testing quality.
 Vehicle Network Test KitRegarding acceptance criteria, reduce rework, allowing OEMs to accept with greater confidence and suppliers to submit with greater peace of mind.
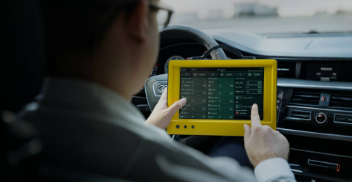 ECU HIL Test PadUniversal Vehicle Body Electronic Environment Simulation System, versatile for multiple uses, rapid screening, ensuring "zero" defects in products.
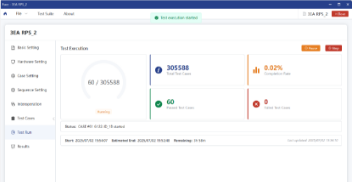 CAN Fuzz Testing AppEfficient, precise, and comprehensive. Your on-the-go vehicle communication security testing expert.


 400 676 5650